Introduction
Manufacturing of pressure vessels requires the integration of good quality welds, high accuracy, productivity, traceability, and process control. With the growth in production volume, lack of skilled labor, stringent quality control measures, and the need to cut down on manufacturing cost of pressure vessels, welding automation has become very essential.
Welding automation in pressure vessels employs the use of mechanized welding, robotics, positioners, manipulators, sensors, welding power source, seam tracking, and digitization of processes to provide consistent welds on repetitive or complex pressure vessels joint.
The goal is not only to increase speed but to have a controlled welding process to give consistent welds which can be traced.
In order to manufacture pressure vessels to ASME standard, there must be the integration of the process with the necessary construction, welding, qualification, inspection and quality control measures. ASME BPVC materials include Section VIII on pressure vessel construction and Section IX on welding, brazing, and fusing qualification.
What Is Welding Automation for Pressure Vessels?
Welding automation can be said to be a systematic approach of conducting welding activities through machinery rather than conducting torch movements through manual operations.
Below are some of the fields where welding automation can be applied during the fabrication of pressure vessels:
• Longitudinal shell welding
• Circumferential shell welding
• Joining of heads and shells
• Nozzles welding
• Reinforcements
• Accessories both internal and external
• Heavy walls
• Special stainless steel fabrication
• Cladding & Overlays
Some of the methods of automation include:
• Mechanical welding carriage
• Robotic welding cells including seam tracking, automated positioning, process control and data acquisition
The most appropriate method depends on the above factors.
Why Automate Pressure Vessel Welding?
1. Higher Productivity
Automation in welding allows for constant and uniform speed as well as welding conditions without getting fatigued like in the case of manual welding.
Efficiency gains may be attained by way of:
• Increased deposition rate
• Increased duration of weld
• Concentration of speed
• Less variance during setup
• Mechanization of positioning
• Less rework
• More efficient use of welding equipment
For heavier fabrication works, processes like the Submerged Arc Welding may allow for higher deposition rate.
2. Consistent Weld Quality
One of the main benefits of automation is repeatability.
The system is able to control or regulate the following:
• welding current,
• arc voltage,
• wire feed rate,
• travel rate,
• torch location,
• oscillation,
• welding order,
• start and end criteria,
• preheating and interpass temperature.
It is possible to decrease variability between operators and increase ability to replicate an approved welding procedure on several vessels.
Nevertheless, it does not mean that automation provides quality. Improper joint preparation, bad programming or fit-up will provide the same problem constantly.
3. Lower Rework Costs
Pressure vessel weld repair will result in high costs due to welding, nondestructive examination (NDE), inspection, documentation, and production time.
Automation would aid in reducing repeated problems such as:
• Undercut
• Lack of fusion
• Inconsistent penetration
• Overreinforcement
• Inconsistent bead shape
• Inconsistent speed
• Arc stability
Thus, first-pass weld quality must always be the priority rather than just high welding speed.
Welding Processes Used in Pressure Vessel Automation
Submerged Arc Welding — SAW
SAW is one of the key automated welding methods for large pressure vessels.
SAW is especially suitable for the following:
• thick carbon steel shells,
• longitudinal joints,
• circumferential joints,
• large diameter vessels,
• application of high deposition.
SAW has stable submerged arc and is very compatible with mechanization.
Modern equipment allows:
• single wire SAW,
• twin wire SAW,
• tandem wire SAW,
• multi-wire application.
The selected method should be accompanied by the proper welding procedure.
Gas Metal Arc Welding — GMAW
Automated GMAW is advantageous in situations where flexibility and accessibility are key considerations.
Examples are:
• Nozzles
• Accessories
• Pads
• Moderately thick parts
• Robotically operated welding cells
Advantages are:
• Continuous feeding of wire
• Parameter programming capabilities
• Good interface with robots
Considerations are gas shielding and fit up of the joint.
Flux-Cored Arc Welding — FCAW
FCAW has good deposition rate capacity and is generally considered for heavy fabrication.
Automated FCAW may be used for:
• Striking and capping passes
• Fabrication attachments
• Carbon and low-alloy steels
• Mechanized welding
As in any automated procedure, the production variables must stay within the limits of the qualified process range.
Gas Tungsten Arc Welding — GTAW
GTAW offers great control and is often preferred for critical root passes, stainless steel, nickel alloy welding, and applications where high-quality welds are desired.
The only drawback to GTAW is its low deposition rate when compared to processes like SAW and FCAW.
In such a case, hybrid processes may offer an advantage, such as using controlled GTAW for the root and another process for the fill.
Automated Longitudinal Seam Welding
Among the most promising longitudinal shell seams suitable for automation are:
• Automated welding carriage
• Automated welding head
• Power supply
• Wire feeder
• Seam tracking system
• Flux delivery system, when needed
• Shell support
• Control of start/stop
• Process control
It is essential that the quality of the previous plate-forming and fit-up procedure be high.
For automation to work best:
• The root gap must be constant;
• The joint alignment must be stable;
• The plate edges must be precisely machined;
• The tacking must be uniform;
• The shell shape must be within specs.
The machine should not have to accommodate forever poor fabrication.
Automated Circumferential Welding
Circumferential welding represents another significant automation application.
Usually, the vessel rotates using rotators powered by motors, whereas the welding torch remains at the proper distance from the weld joint.
The following parameters need to be coordinated:
Vessel rotation + torch motion + welding process parameters + seam tracking.
Among factors to take into account, there are:
• Diameter of the vessel
• Roundedness
• Mismatch
• Root opening
• Welding position
• Torch angle
• Speed of travel
• Torch orientation
For large vessels, rotators and work piece handling system are essential parts of an automation system.
Robotic Welding for Pressure Vessels
Robotic welding has more flexibility than that of the specialized mechanized tool.
Components in the robotic welding cells of pressure vessels may consist of:
• Multi-axis industrial robot
• Welding power supply
• Wire feeder
• Positioner
• Rotator
• Seam tracker
• Laser/vision sensor
• PLC
• HMI
• Safety system
• Fume removal
• Data acquisition
It is especially useful in companies that have several types of vessels and complicated nozzle and attachment configuration.
The robot is just one component of the complete system.
The welding procedure, joint preparation, fixtures, sensors, programming, inspection, and quality system determine the actual manufacturing capability.
Seam Tracking and Weld Joint Detection
One of the biggest problems with automated welding is that the physical joint seldomly aligns perfectly with the theoretical joint CAD design.
Sources of variation can be any of the following:
• Plate formation
• Weld shrinkage
• Thermal distortion
• Root gap variation
• Fit up
• Tack Welding
• Dimensional tolerance
The seam tracking technology allows the welding head to identify the joint in question.
The most common techniques are:
Laser Tracking
Employs laser sensors to measure joint geometry and location.
Through Arc Tracking
Employ changes in weld signal as an indication of lateral deviation from joint location.
Touch Sensing
Employ welding process for locating physical part prior to welding.
Vision System
Employ cameras and image processing algorithms to locate joint geometry and welding conditions.
In cases of valuable pressure vessel production, seam tracking will greatly enhance repeatability of the process..
WPS, PQR and ASME Welding Requirements
Automation does not eliminate welding qualification requirements.
For ASME-governed manufacturing, Section IX is central to welding, brazing, and fusing qualifications, while Section VIII addresses applicable pressure-vessel construction requirements. ASME’s current BPVC catalog identifies Section IX as the qualification standard and Section VIII divisions as pressure-vessel construction standards.
A production automation program should therefore be developed around the approved welding procedure.
Important variables may include:
- Welding process
- Base material
- Thickness
- Filler metal
- Joint design
- Welding position
- Current
- Voltage
- Travel speed
- Heat input
- Preheat
- Interpass temperature
- Shielding gas
- Welding technique
- Post-weld heat treatment where applicable
The automated system must reproduce the required process within the applicable qualified range.
Heat Input, Preheat and Interpass Control
Heat management is important when it comes to pressure vessel welding, since it may affect the following factors:
• Microstructure
• Hardness
• Toughness
• Distortion
• Stresses
• HAZ properties
• Cracking tendency
An example of simplified heat input calculation is the following one:
Heat Input ≈ (Voltage × Current × 60) / (Travel Speed × 1000)
The correct heat input formula should be selected based on the welding procedure specifications and requirements.
Current, voltage, and travel speed can all be tracked automatically, giving much more insight into the process than the manual calculations could do.
Temperature tracking equipment may also be used for preheating and interpass temperature measurement.
Welding Automation and NDE
Automation contributes to process consistency, although automation does not replace inspection.
Depending on the requirements in the applicable design and inspection, pressure vessel welds may need testing procedures like:
· Visual Testing
· Radiographic Testing
· Ultrasonic Testing
· Phased Array UT
· TOFD
· Magnetic Particle Inspection
· Liquid Penetrant Inspection
According to ASME, Section V is designated as the BPVC section for Nondestructive Examination and is included in the list of code resources for pressure-vessel certification programs.
The important point is:
· Process monitoring ensures how the weld was made.
· NDE tests the outcome of the process according to the inspection requirements.
Both of them are important.
Digital Traceability in Automated Welding
Contemporary pressure vessel manufacturers are making efforts to integrate welding machines with digital quality systems.
A digital weld record may contain:
Vessel → Joint → Material → WPS → Welding program → Consumable → Operator → Welding parameters → NDE → Inspection
The following parameters can be potentially recorded:
• Current
• Voltage
• Travel speed
• Wire-feed speed
• Arc time
• Temperature
• Program number
• Vessel serial number
• Joint number
• Operator ID
• Alarm history
• Equipment identification
In that way, manufacturers have a digital manufacturing history for every vessel.
In case when a manufacturer operates within a formal quality system, digital traceability will help to achieve better document management, analysis of production, audit readiness, and quality investigations.
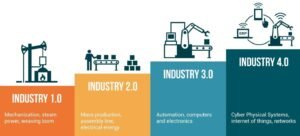
AI and Industry 4.0 in Pressure Vessel Welding
The future direction of automation of the welding process will go from robot programming into the manufacturing based on data.
The potential applications of AI include analysis of dependencies between:
• Welding parameters,
• Signals from arc,
• Temperature,
• Geometry of joint,
• Information from sensors,
• History of defects,
• NDE results.
Predictive quality,
Prediction of the process conditions leading to higher defect rate.
Anomaly detection,
Real-time detection of unusual welding.
Predictive maintenance,
Detection of unusual conditions in robots, wire feeding systems, positioners, power supplies, and other equipment.
Process optimization,
Analysis of manufacturing data for improvement of productivity while maintaining approved process windows.
AI should be considered as an additional layer of manufacturing intelligence but not a substitute for qualified welding engineering and inspection.
How to Select a Pressure Vessel Welding Automation System
- Prior to implementing automation technology, the manufacturer needs to consider the entire production process.
1. Vessel Dimensions
Determine min and max:
• Diameter
• Length
• Weight
• Wall thickness
2. Material Selection
Look at:
• Carbon steel
• Low-alloy steel
• Stainless steel
• Nickel alloys
• Cladding materials
3. Type of Joints
Determine the percent of production:
• Longitudinal joints
• Circumferential joints
• Nozzles
• Heads
• Attachments
4. Production Quantity
High quantity repetitive production is usually ideal for dedicated automation.
High mix production can be justified for using flexible robotic solutions.
5. Quality Requirements
The system must be capable of providing:
• Process control
• Inspection
• Traceability
• Data collection
• Documentation of quality
6. Future Additions
Think about the ability of adding:
• Seam tracking
• Vision
• MES
• Automated inspection
• Weld digital records
• Predictive maintenance
ROI of Welding Automation
The business case should not be based solely on labor reduction.
A more complete calculation considers:
Automation Benefit =
Productivity gain
- labor efficiency
- reduced rework
- reduced consumable waste
- lower downtime
- improved throughput
- improved traceability
- safety improvements
Against:
Automation Cost =
Equipment
- integration
- programming
- training
- maintenance
- software
- fixtures
- facility modifications
- calibration
- downtime
A particularly useful manufacturing KPI is:
Cost per conforming weld
rather than simply cost per welding hour.
A system that welds rapidly but generates excessive repairs may have poor overall economics.
Common Automation Challenges
Poor Fit-Up
Inconsistency of root gap width and joint alignment will significantly degrade automation capabilities.
Highly Variable Product
The custom-made machine will be rendered less efficient if each container has to be programmed differently.
Poor Programming
Improper programming of robot paths and/or weld parameters will cause consistent defects.
Poor Upstream Control
Automation cannot fix bad plate forming, machining, and assembly forever.
Unskilled People
Robotics still needs welding engineers, programmers, mechanics, inspectors, and maintenance people.
Poor Data Management
Modern welding station generates valuable production data. Without proper data management structure, most of this data goes wasted.
Pressure Vessel Welding Automation Trends in 2026
The pressure vessel production industry is shifting towards more extensive automation through:
• Robotic welding
• Laser seam tracking
• Machine vision
• Real-time monitoring of parameters
• Temperature control systems
• Weld data digitalization
• MES integration
• Predictive maintenance
• Quality analysis using AI
• Inspection automation
• Digital twin technology
In the future, the key to success will be linking all these technologies in one manufacturing process.
The aim is not just:
“To automate the welding process.”
The aim will be:
“To digitally manage and monitor the whole welding process.”
Pressure Vessel Welding Automation: Final Takeaway
Welding automation is emerging as a manufacturing strategy that could help pressure vessel manufacturers become more productive without losing process control.
Some of the best automation technologies include:
Proven welding procedure specification + proper fit-up + automated welding + seam tracking + temperature control + inspection + digital traceability + competent engineers.
SAW has proven itself to be very attractive in case of long and heavy welding, while robotized GMAW, FCAW, and GTAW systems give flexibility in terms of manufacturing of complex parts and various material application.
For manufacturing processes regulated by ASME, the automation must still be consistent with BPVC standards, welding qualification, examination, quality management system, and project specifications. ASME BPVC resources currently available place Sections VIII, IX, V and relevant material requirements at the core of any applicable pressure vessel certification scheme.
In summary, the effectiveness of welding automation lies in the capacity of the manufacturer to produce high-quality, traceable and conforming pressure vessels at a reasonable price rather than in the technological prowess of the robot.
Frequently Asked Questions
What is welding automation for pressure vessel manufacturing?
It is using mechanized or robotic welding equipment, welding controls, sensors, positioners, and monitoring systems to create pressure-vessel welds with predictable and consistent parameters.
Which welding process is most suitable for pressure vessels?
There is no single answer. For example, SAW often produces excellent results in long and thick-section seams, while GMAW, FCAW, and GTAW may be preferable in certain situations.
Is full automation possible for pressure vessel welding?
Much of repetitive welding processes can be automated effectively. But engineering, fit-up, inspection, maintenance, programming, quality control, and code compliance still remain the responsibility of professionals.
Is welding procedure specification required for robotic welding?
If the construction code calls for a welding procedure specification, robotic or automated welding does not make the qualification obsolete. The automated production system must run according to qualified parameters.
Can AI be used as a substitute for pressure vessel welding inspection?
Absolutely not. AI can help monitor the process, identify abnormalities, and perform visual inspections, but it cannot be considered as a substitute for required NDE.
Why does welding automation reduce the cost of manufacturing?
The main benefits are increased efficiency, decreased variability, lower rework, improved equipment utilization, material efficiency, and enhanced production traceability.
What is the main requirement for welding automation to work well?
Process stability. It is crucial to have consistent material preparation, joint fit-up, welding procedures, equipment setup, positioning, and inspection in place prior to automation.